5-Axis and Wire EDM Machined Stainless Steel Components
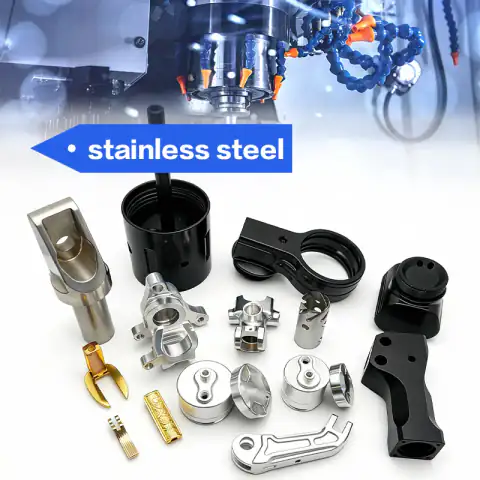
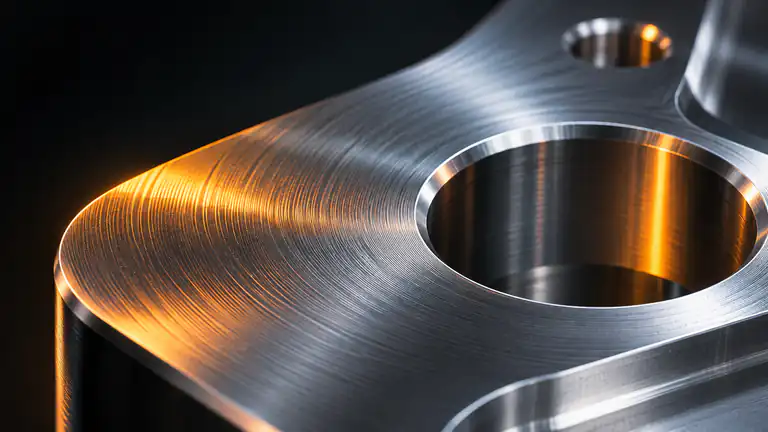
These are stainless steel components that need both 5-axis milling and wire EDM: for example, a contoured body with a narrow slot, a gear profile or a sharp-cornered internal window. Milling produces the 3D shape efficiently, and EDM cuts the features no cutter can reach. The service suits industrial machine designers and automation builders needing intricate stainless parts.
- Material
- Stainless Steel
- Tolerance
- to ±0.005 mm
- MOQ
- 1 piece
- Prototype lead time
- 3–7 days
- 5-axis milled shape plus EDM-cut fine features
- 17-4PH hardened before EDM for wear resistance
- Sharp internal corners and narrow slots
- Optical or CMM profile verification
Item ref. 1601360685905 ·
| Process | 5-axis CNC milling, wire EDM, drilling, passivation |
|---|---|
| Materials | Stainless steel 17-4PH, 303, 304, 316 |
| Surface Finish | As machined, EDM finish with skim cuts, passivation, bead blasting |
| Tolerance | ±0.05 mm standard; down to ±0.005 mm on critical features |
| MOQ | 1 piece; prototypes through mid-volume runs |
| Drawing Formats | STEP, IGES, X_T, STL, DWG, DXF, PDF |
| Lead Time | Prototypes typically 3–7 working days; production usually 10–20 |
| Inspection | FAI, in-process checks, 100% critical dimensions; CMM |
Manufacturing
How we make this part
Process, material options and inspection for 5-axis and wire edm machined stainless steel components.
The usual sequence is to rough and finish the outer geometry on a 5-axis mill, drill EDM start holes, then transfer to the wire EDM machine with a fixture that references the milled datums. Wire EDM cuts through-slots, keyways, small gear teeth or internal profiles without mechanical force. Any final milling of faces affected by EDM fixturing is done last.
17-4PH stainless is often chosen because it can be hardened to around 40 HRC before EDM cutting, giving strong, wear-resistant profiles. 304 and 316 suit parts needing corrosion resistance without hardness. 303 helps when much milling is involved. Wire EDM leaves a matte surface; additional skim cuts improve finish. Passivation after machining removes surface contaminants.
Profile accuracy is checked with optical measurement or CMM; slot widths with pin gauges. Each part is inspected on critical dimensions, and reports are supplied on request. Typical components include indexing plates, gripper fingers, cam followers, small gears, cutter blades, latch mechanisms and precision guides for packaging, textile and automation machinery.
FAQ
Frequently asked questions
Can wire EDM cut hardened 17-4PH stainless steel?
Yes. Wire EDM cuts any conductive metal regardless of hardness. 17-4PH can be aged to its required condition first, and then profiles are cut by EDM, avoiding distortion from heat treatment after finishing. This is common for gripper fingers, cams and wear parts.
Why combine 5-axis milling and wire EDM on one part?
Each process handles what it does best. Milling quickly creates 3D shapes, pockets and surfaces; wire EDM produces sharp internal corners, narrow slots and precise through-profiles that cutters cannot. Combining them in one shop keeps datums consistent and avoids shipping parts between suppliers.
How do I get a quote for 5-axis and wire edm machined stainless steel components?
Send a 3D model (STEP or IGES) and a 2D drawing with tolerances, material, finish and quantity through the quote form or by email. An engineer replies within 24 hours on business days with price, lead time and any DFM suggestions.
Request a quote
Quote this part
Attach drawings or send several parts at once from the full quote form.
- Email[email protected]
- WhatsApp+86 176 2154 1688
- Phone+86 176 2154 1688
- HoursMon–Sat, 08:30–18:00 China Standard Time (UTC+8)