5-Axis CNC Milled Aluminum Suspension Knuckle
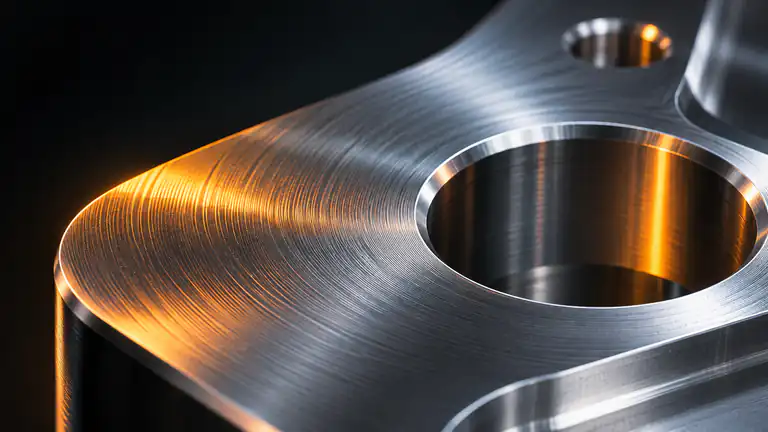
This is a 5-axis CNC milled aluminum suspension knuckle, or upright, for automotive chassis and motorsport applications. It is machined from 6061 or 7075 billet, or finished from a forging, with hub bearing bores, ball joint tapers, caliper mounts and steering arm holes. It suits race car builders, EV prototype teams and chassis developers who need low-volume knuckles to their own geometry.
- Material
- Aluminum
- Tolerance
- to ±0.005 mm
- MOQ
- 1 piece
- Prototype lead time
- 3–7 days
- Angled features machined in minimal setups
- Hub bearing bores finish-bored for press fits
- 7075 or 6061 billet, or machined forgings
- CMM-verified geometry on first articles
Item ref. 1601926462749 ·
| Process | 5-axis CNC milling, boring, taper cutting, drilling |
|---|---|
| Materials | Aluminum 7075-T6, 6061-T6; forged blanks on request |
| Surface Finish | Hard anodizing, Type II anodizing, masking of bearing seats |
| Tolerance | ±0.05 mm standard; down to ±0.005 mm on critical features |
| MOQ | 1 piece; prototypes through mid-volume runs |
| Drawing Formats | STEP, IGES, X_T, STL, DWG, DXF, PDF |
| Lead Time | Prototypes typically 3–7 working days; production usually 10–20 |
| Inspection | FAI, in-process checks, 100% critical dimensions; CMM |
Manufacturing
How we make this part
Process, material options and inspection for 5-axis cnc milled aluminum suspension knuckle.
Knuckles have features on many angled faces, so 5-axis machining is the practical route: the bearing bore, brake caliper mounts, ball joint seats and tie-rod holes are cut in as few setups as possible, keeping their geometric relationships tight. Bores are finish bored for bearing press fits, and tapers are cut with form tools or interpolation.
7075-T6 offers high strength for motorsport uprights; 6061-T6 is easier to machine and anodize and suits lighter vehicles or prototypes. Forged blanks give better grain flow and fatigue strength than billet for production. Hard anodizing protects bearing bores, though those seats are often masked to keep press-fit tolerance. Steel inserts can be added for threads that are frequently serviced.
Bearing bores, caliper mounting hole positions and kingpin or ball joint geometry are measured with CMM on first articles, and critical dimensions are inspected on every part. Material certificates are supplied on request. Typical applications include Formula Student uprights, race car knuckles, EV and kit car chassis prototypes, UTV front knuckles and low-volume replacement parts.
FAQ
Frequently asked questions
Billet or forged aluminum for suspension knuckles?
Billet is ideal for prototypes and very low volumes because no forging die is needed. Forged blanks have grain flow that follows the part shape, improving fatigue strength, and they cut machining time, so they pay off at higher volumes. Many programs prototype in billet and switch to forgings for production.
Do you do strength or fatigue testing on knuckles?
We control the machined geometry and supply dimensional reports and material certificates. Structural validation, such as FEA, fatigue or proof testing, is the vehicle designer's responsibility. We can supply extra parts for your testing and machine any test fixtures needed.
How do I get a quote for 5-axis cnc milled aluminum suspension knuckle?
Send a 3D model (STEP or IGES) and a 2D drawing with tolerances, material, finish and quantity through the quote form or by email. An engineer replies within 24 hours on business days with price, lead time and any DFM suggestions.
Request a quote
Quote this part
Attach drawings or send several parts at once from the full quote form.
- Email[email protected]
- WhatsApp+86 176 2154 1688
- Phone+86 176 2154 1688
- HoursMon–Sat, 08:30–18:00 China Standard Time (UTC+8)