5-Axis CNC Milled Multi-Face Aluminum Housings
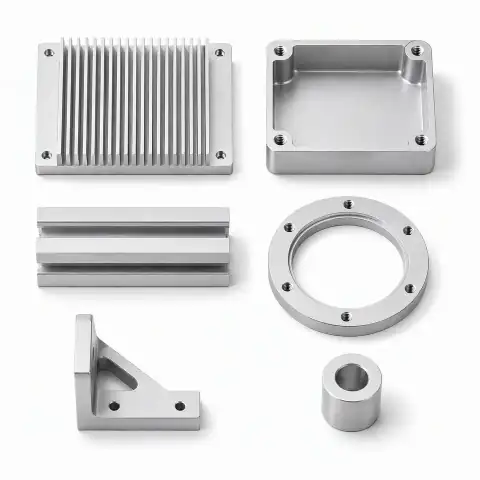
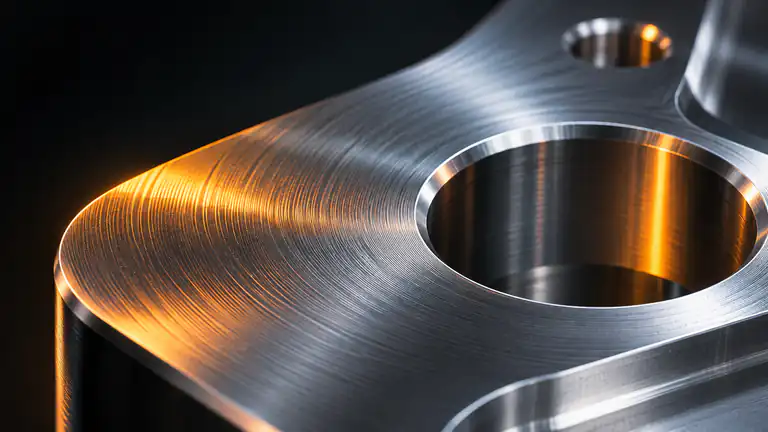
These are multi-face aluminum housings produced by 5-axis CNC milling: gearbox cases, sensor bodies, valve blocks, instrument housings and connector shells with features on five or six sides. Machining several faces in one setup keeps hole positions accurate between them. The service suits engineers whose parts would otherwise need many fixtures and setups on 3-axis machines.
- Material
- Aluminum
- Tolerance
- to ±0.005 mm
- MOQ
- 1 piece
- Prototype lead time
- 3–7 days
- Five faces machined in one clamping
- Angled holes cut without special fixtures
- CMM verification of cross-face hole positions
- 6061-T6, 7075-T6, 6063, stainless or brass
Item ref. 1601677991498 ·
| Process | 5-axis CNC milling, drilling and tapping |
|---|---|
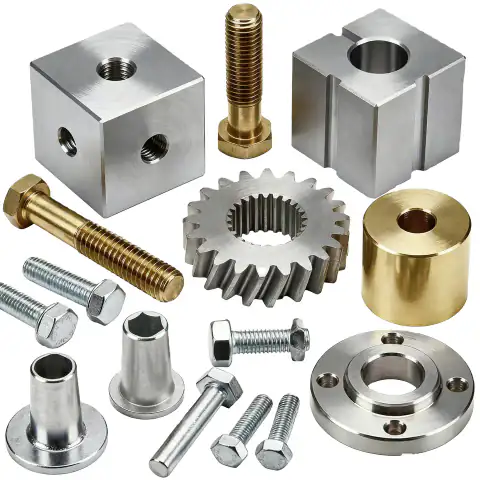
| Materials | Aluminum 6061-T6, 7075-T6, 6063; stainless steel 304; brass |
| Tolerance | ±0.05 mm standard; down to ±0.005 mm on critical features |
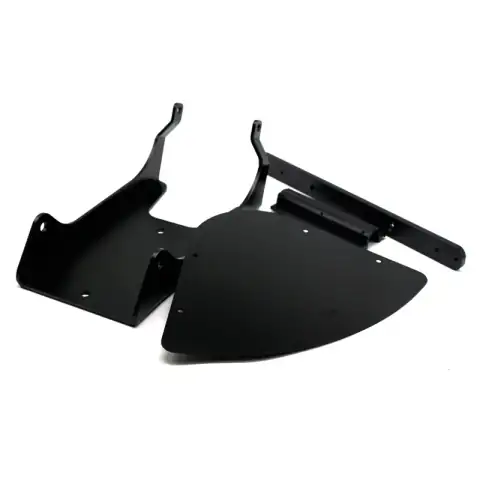
| Surface Finish | Type II / Type III anodizing, powder coating, conductive coating |
| Typical Parts | Sensor bodies, valve blocks, gearbox cases |
| MOQ | 1 piece; prototypes through mid-volume |
| Drawing Formats | STEP, IGES, X_T, STL, DWG, DXF, PDF |
| Lead Time | Prototypes typically 3–7 working days; production 10–20 |
| Inspection | First-article, in-process and CMM checks; reports on request |
Manufacturing
How we make this part
Process, material options and inspection for 5-axis cnc milled multi-face aluminum housings.
A housing with ports on several sides often needs four to six setups on a 3-axis mill, and each re-clamp adds positional error. On a 5-axis machine, the part is held once on a fixture or dovetail stub and the spindle reaches five faces, with only the base finished in a second operation. Angled holes and compound surfaces are cut directly without special angle fixtures.
6061-T6 is the default housing alloy for its machinability and anodize quality; 7075-T6 suits thin-walled, high-stress housings; 6063 is used when parts start from extrusion. Stainless steel and brass can be machined the same way when corrosion or conductivity requires it. Finishes include Type II color anodizing, hard anodizing, powder coating and conductive chromate-free coatings where grounding is needed.
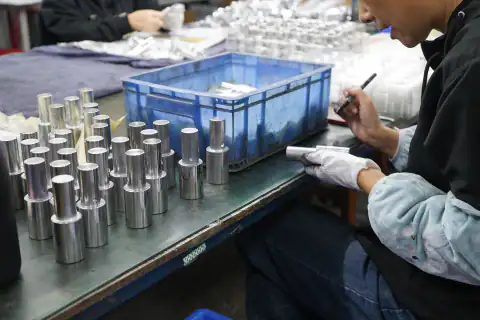
Hole positions across faces are measured on a CMM, since that relationship is the main reason to choose 5-axis. Threads are checked with gauges and sealing faces for flatness. The first article is fully reported before production. Typical housings include sensor and camera bodies, hydraulic and pneumatic valve blocks, small gearbox cases and optical instrument frames.
FAQ
Frequently asked questions
Is 5-axis machining more expensive than 3-axis?
The hourly machine rate is higher, but for multi-face housings the total cost is often similar or lower, because one or two setups replace four to six. Fewer setups also reduce fixture cost, handling and the risk of positional errors, which can make 5-axis the better value.
Can you machine housings from extrusion instead of solid block?
Yes. If the housing shape is close to a standard or custom extrusion, starting from 6063 or 6061 extrusion saves material and machining time. We then machine ports, pockets and mounting features on the 5-axis center. We can advise whether your design suits this.
How do I get a quote for 5-axis cnc milled multi-face aluminum housings?
Send a 3D model (STEP or IGES) and a 2D drawing with tolerances, material, finish and quantity through the quote form or by email. An engineer replies within 24 hours on business days with price, lead time and any DFM suggestions.
Request a quote
Quote this part
Attach drawings or send several parts at once from the full quote form.
- Email[email protected]
- WhatsApp+86 176 2154 1688
- Phone+86 176 2154 1688
- HoursMon–Sat, 08:30–18:00 China Standard Time (UTC+8)