Simultaneous 5-Axis CNC Machined Complex Contour Parts
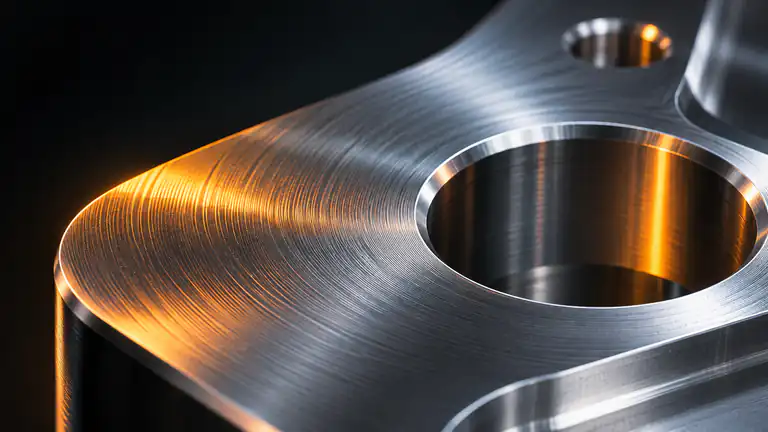
This service uses simultaneous 5-axis CNC milling to produce parts with complex freeform surfaces: impellers, blade profiles, ergonomic handles, aerodynamic fairings, mold cores and medical-style contoured components. All five axes move together, keeping the tool normal to the surface. It is meant for designers whose parts cannot be cut accurately with 3+2 positional machining.
- Material
- Aluminum
- Tolerance
- to ±0.005 mm
- MOQ
- 1 piece
- Prototype lead time
- 3–7 days
- Tool angle changes continuously along the path
- Short, rigid tools on twisted blade surfaces
- Ra 0.8–1.6 µm achievable on many contours
- CMM comparison of surfaces to CAD model
Item ref. 1601683106358 ·
| Process | Simultaneous 5-axis CNC milling |
|---|---|
| Materials | Aluminum 6061, 7075; stainless steel 304, 17-4PH; titanium Gr5 |
| Tolerance | ±0.05 mm standard; down to ±0.005 mm on critical features |
| Surface Finish | As-machined, polishing, anodizing, bead blasting |
| Surface Roughness | Ra 0.8–1.6 µm typical as-machined on contours |
| MOQ | 1 piece; prototypes through mid-volume |
| Drawing Formats | STEP, IGES, X_T, STL, DWG, DXF, PDF |
| Lead Time | Prototypes typically 3–7 working days; production 10–20 |
| Inspection | First-article, in-process and CMM checks; reports on request |
Manufacturing
How we make this part
Process, material options and inspection for simultaneous 5-axis cnc machined complex contour parts.
In 3+2 machining the part is tilted to a fixed angle and then cut with three axes; in simultaneous 5-axis, the tool angle changes continuously along the path. That lets a short, rigid tool follow twisted surfaces such as impeller blades without hitting neighboring features. The result is better surface finish, fewer witness lines between patches and less hand polishing afterward.
Aluminum 6061 and 7075 cut quickly and suit prototypes, fans and fairings. Stainless steel and 17-4PH are used for pump impellers that see corrosion. Titanium Gr5 is chosen for lightweight high-strength parts but needs lower cutting speeds and rigid setups. Surface finishes around Ra 0.8–1.6 µm are achievable directly from the machine on many contours, with polishing for mirror finishes.
Freeform surfaces are verified against the CAD model on a CMM, comparing measured points to nominal geometry, and blade thickness or critical profiles can be reported. Every critical dimension is checked before shipment. Typical parts include centrifugal impellers, drone propeller prototypes, turbine blade models, ergonomic tool handles, mold inserts and orthopedic-style contour samples.
FAQ
Frequently asked questions
What is the difference between 3+2 and simultaneous 5-axis?
In 3+2 machining, the part is tilted to fixed angles and cut with three moving axes, which suits prismatic parts with angled faces. Simultaneous 5-axis moves all axes at once, so the tool can follow twisted freeform surfaces such as impeller blades with a constant engagement and better finish.
Can you machine an impeller from a single block?
Yes. Closed or open impellers are often cut from one solid block of aluminum, stainless steel or titanium on a simultaneous 5-axis machine. Blade spacing and depth decide the smallest tool we can use, so very tight blade passages may require design review before quoting.
How do I get a quote for simultaneous 5-axis cnc machined complex contour parts?
Send a 3D model (STEP or IGES) and a 2D drawing with tolerances, material, finish and quantity through the quote form or by email. An engineer replies within 24 hours on business days with price, lead time and any DFM suggestions.
Request a quote
Quote this part
Attach drawings or send several parts at once from the full quote form.
- Email[email protected]
- WhatsApp+86 176 2154 1688
- Phone+86 176 2154 1688
- HoursMon–Sat, 08:30–18:00 China Standard Time (UTC+8)