Wire EDM Cut Stainless Steel and Aluminum Lighting Parts
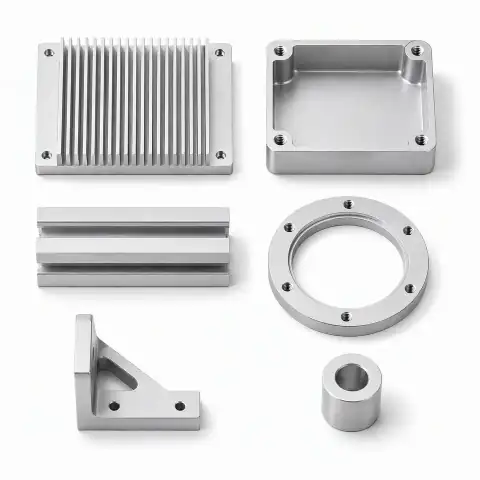
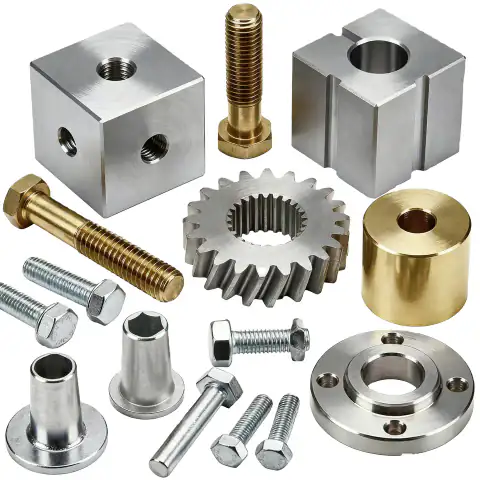
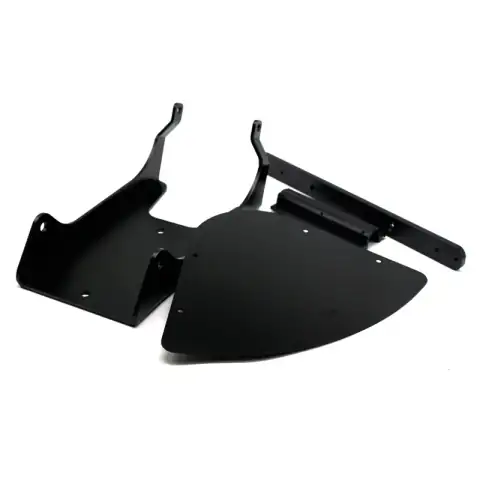
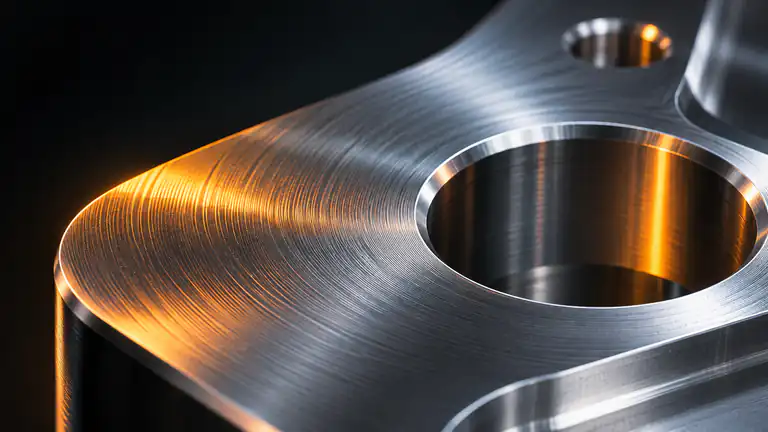
These are precision lighting parts made by wire EDM and CNC machining from stainless steel, aluminum and titanium. Wire EDM cuts fine slots, louvers, patterned plates and sharp-cornered openings that conventional milling cannot achieve. CNC machining completes outer shapes, threads and mounts. The service suits lighting manufacturers and designers needing intricate metal parts for fixtures and optics.
- Material
- Stainless Steel
- Tolerance
- to ±0.005 mm
- MOQ
- 1 piece
- Prototype lead time
- 3–7 days
- Fine slots and patterns cut by wire EDM
- Stacked cutting for identical plates
- Narrow deep heat sink fins without long tools
- Stainless, aluminum and titanium options
Item ref. 1601377668185 ·
| Process | Wire EDM, CNC milling, CNC turning |
|---|---|
| Materials | Stainless steel 304, aluminum 6061, titanium Gr2/Gr5 |
| Surface Finish | Anodizing, passivation, black finishes, PVD |
| Tolerance | ±0.05 mm standard; down to ±0.005 mm on critical features |
| MOQ | 1 piece; prototypes through mid-volume runs |
| Drawing Formats | STEP, IGES, X_T, STL, DWG, DXF, PDF |
| Lead Time | Prototypes typically 3–7 working days; production usually 10–20 |
| Inspection | FAI, in-process checks, 100% critical dimensions; CMM |
Manufacturing
How we make this part
Process, material options and inspection for wire edm cut stainless steel and aluminum lighting parts.
Thin plates are cut by wire EDM with very fine slots and complex patterns, including multiple parts stacked in one cut. Thicker heat sinks can have narrow, deep fins cut by EDM where milling tools would be too long. CNC machining adds mounting holes, threads and outer profiles. Parts are cleaned to remove EDM residue and deburred.
Stainless steel 304 resists heat and corrosion and suits louvers and frames; aluminum 6061 is lighter and conducts heat for fins and housings; titanium is used for special decorative pieces. EDM surfaces are matte and burr-free. Aluminum is anodized after EDM cutting; stainless can be passivated, blackened or PVD coated to reduce glare.
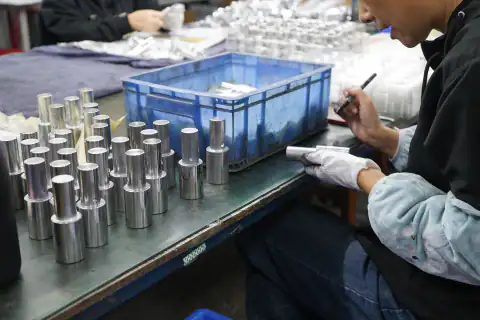
Slot widths, pattern positions and outer dimensions are checked with optical measurement and CMM, and critical features are inspected before shipping. Typical uses include glare-control louvers, honeycomb-style frames, decorative patterned plates, light-shaping masks, fine-fin heat sinks and precision lens retainers for lighting fixtures, in prototype or batch quantities for architectural, stage and retail lighting brands.
FAQ
Frequently asked questions
How narrow can wire EDM slots be?
Slot width equals wire diameter plus spark gap, so with fine wire slots around 0.15–0.3 mm are possible, depending on material thickness. Narrow slots in thick material take longer to cut. We will recommend the practical minimum based on your part.
Is wire EDM cost-effective for lighting parts?
For intricate patterns, fine slots or small batches, yes, because no tooling is needed and accuracy is high. For simple shapes in large volumes, laser cutting or stamping is cheaper. Many lighting brands use EDM for prototypes and premium fixtures.
How do I get a quote for wire edm cut stainless steel and aluminum lighting parts?
Send a 3D model (STEP or IGES) and a 2D drawing with tolerances, material, finish and quantity through the quote form or by email. An engineer replies within 24 hours on business days with price, lead time and any DFM suggestions.
Request a quote
Quote this part
Attach drawings or send several parts at once from the full quote form.
- Email[email protected]
- WhatsApp+86 176 2154 1688
- Phone+86 176 2154 1688
- HoursMon–Sat, 08:30–18:00 China Standard Time (UTC+8)